Get Quote
Contact us now to receive a detailed quotation.
Overview
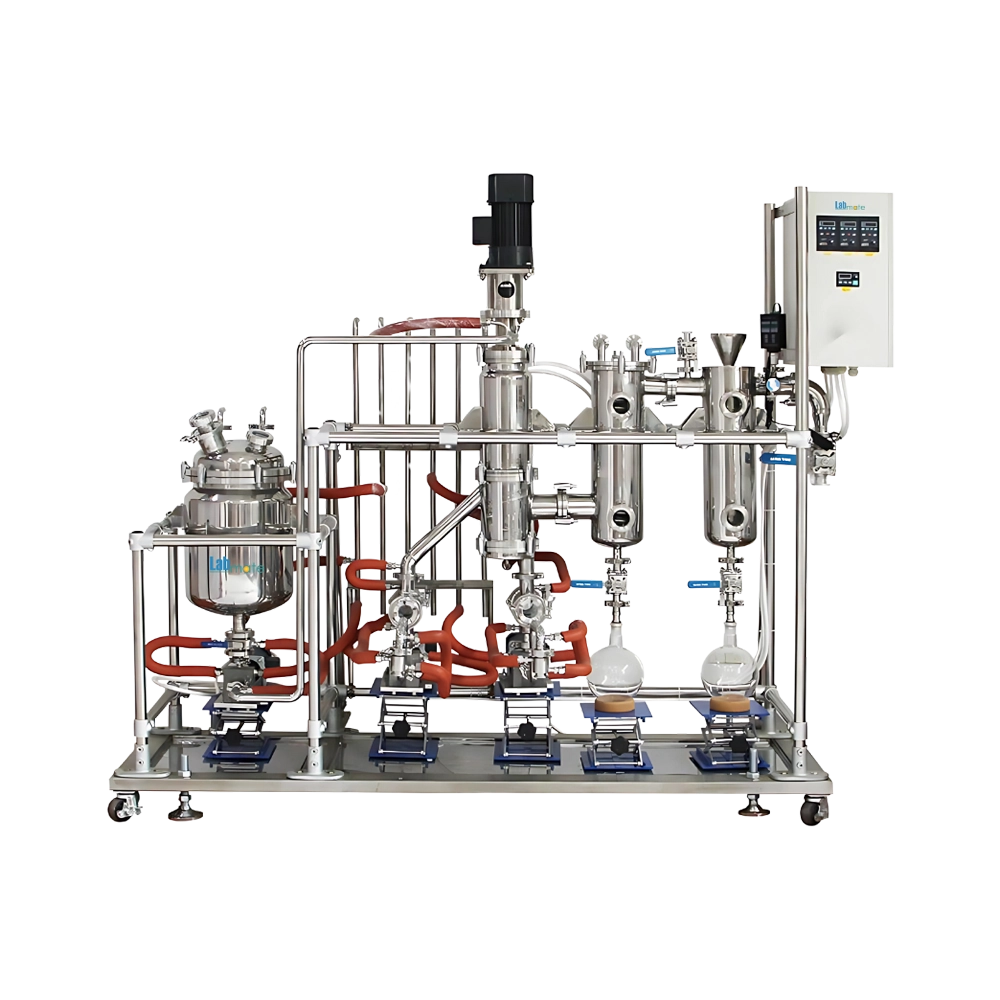
Molecular Distillation Unit LMMDU-A105 is designed with feeding rate of 1.5 to 6 L/h. Its full jacket and insulation design ensure smooth material flow. Equipped with an automatic feeding and discharging pump, it optimizes production capacity. Incorporates magnetic coupling seal for stable vacuum conditions. Our Distiller purifies chemicals, medicines, food, beverages, and petroleum products.
Features :
Preheating feed tank
Blockage prevention
External condenser support
Polished inner wall
Fluororubber sealing
Sight glass monitoring
Continuous operation motor
Specifications :
| Feeding Rate | 1.5 to 6 L/h |
| Feeding Flask Volume | 15 L |
| Operating Temperature | Less than or equal to 350°C |
| Vacuum Level | Less than or equal to 0.01 millibar |
| Material | Stainless steel 316L |
| Evaporation Area | 0.1 m² |
| Power Supply | 220V/50Hz,1P |
| Dimensions | 2350×900×1900 mm |
Applications :
Molecular Distillation Unit LMMDU-A105 ensures separation, purification, and concentration in chemical, pharmaceutical, food, beverage, and petroleum industries for polymers, medicines, dairy, juices, syrups, lubricants, and solvents.
Selection Guide :
Molecular Distillation Unit LMMDU-A105 is best suited for research and industrial applications requiring high-throughput purification of thermally sensitive and high-boiling-point compounds. With a feeding rate of 1.5 to 6 L/h and a large 15 L feeding flask volume, it supports continuous processing of substantial sample quantities, making it suitable for pilot-scale or production-level distillation. Its ability to operate at temperatures up to 350°C and vacuum levels as low as 0.01 millibar ensures efficient separation of compounds with very low vapor pressures. This model is commonly used in pharmaceutical, nutraceutical, chemical, and cannabinoid industries for purifying essential oils, vitamins, fatty acids, and other heat-sensitive materials. When selecting this unit, researchers should consider its compatibility with their volume needs, process scalability, and compliance with GMP and CE certifications, which ensure quality and safety standards for research and regulated production environments.